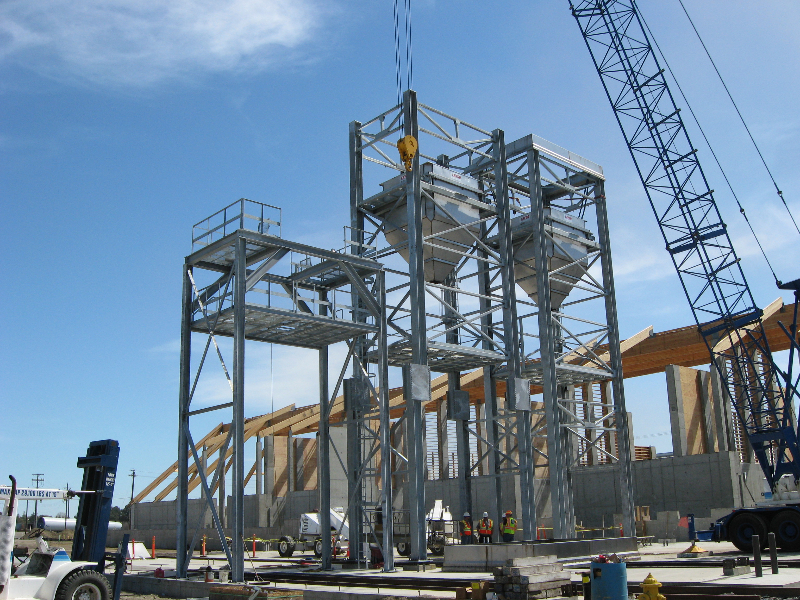
A galvanized structural steel frame being set by crane against a clear sky

Vacaville, California

Court GalvanizingInc.

Hot-dip galvanizing for Northern and Central California, Western Nevada and Southern Oregon — steel that goes out coated to last.

Kettle length25′ 0″Working length
Kettle depth8′ 6″Single dip
Zinc bath850°F98% pure zinc
AssociationAGAMember in good standing

Who we are

Corrosion protection, built into the steel.

Court Galvanizing, Inc. specializes in providing corrosion-resistant hot-dip galvanizing to the Northern and Central California, Western Nevada and Southern Oregon markets.

We have close ties to our community and environment, and we work to our best-in-class delivery, quality, on-time scheduling and price for the corrosion protection needs of the future.

Our mission is to continuously provide the market's highest quality in hot-dip galvanizing, and to stay current with the progression of galvanizing through our affiliation as a proud member in good standing of the American Galvanizers Association.
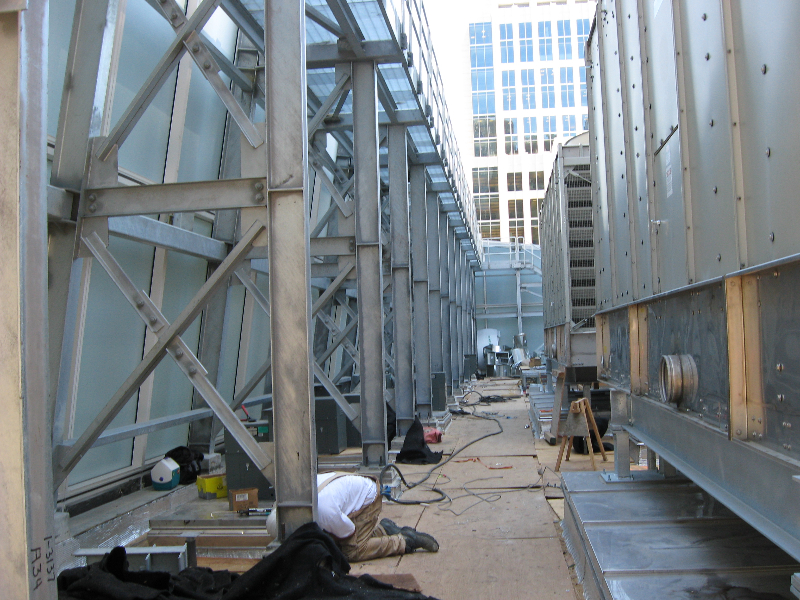
Galvanized structural steel framing and ductwork on a rooftop between office towers
Structural steel, galvanized and set.

The process

Three elements, in order.

Hot-dip galvanizing is a factory-applied molten coating. The primary responsibility for surface preparation, as well as coating application, falls with the galvanizer.

01

Surface preparation

The most critical step. If the steel is not properly cleaned, the zinc will not adhere to it.

  1. Degreasing / caustic cleaning — a heated alkali solution lifts dirt, oil, grease, shop oil and soluble markings.
  2. Acid pickling — dilute heated sulfuric acid removes mill scale and surface rust for a chemically clean surface.
  3. Fluxing — zinc ammonia chloride removes oxides and stops new ones forming before the dip.
02

Hot-dip galvanizing

The material is completely immersed in a bath of 98% pure molten zinc, held at about 850 degrees Fahrenheit.

It stays in long enough to reach bath temperature, then is withdrawn slowly, with excess zinc removed by draining and wiping. The bath chemistry is specified by the American Society for Testing and Materials.

03

Inspection

Quality control — the finished coating is checked against the applicable standards and against the specific requirements of the customer.

Paint, epoxies, vinyls, asphalt or weld slag must be removed by grit or sand blasting before galvanizing; that removal is the fabricator's responsibility.
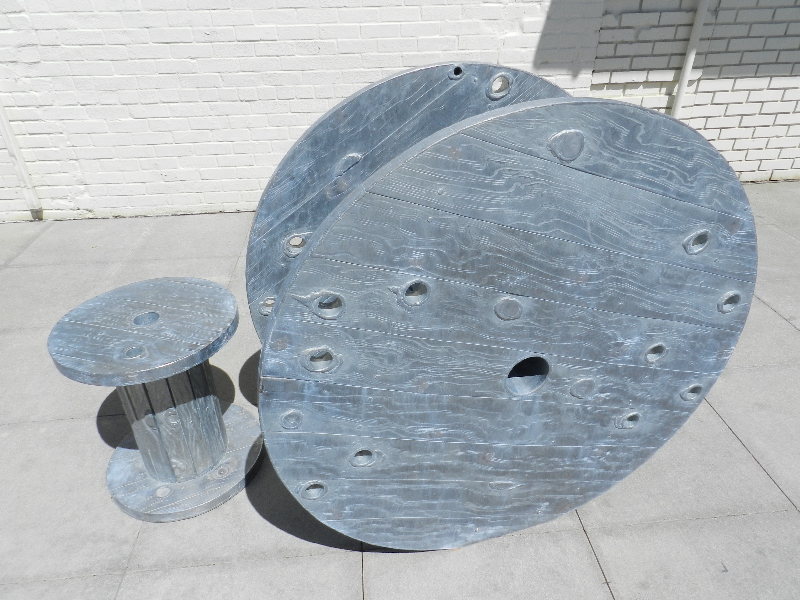
Freshly galvanized steel discs and a spool showing the spangled zinc surface

The kettle

Twenty-five feet of molten zinc.

Knowing the kettle tells you what fits in a single dip — and a single dip is a better coating than a double.

Length25′ 0″
Width3′ 9″
Depth8′ 6″

Work that went out the door.

Structural frames, handrail and guardrail, solar racking, architectural rail — and the occasional sculpture.
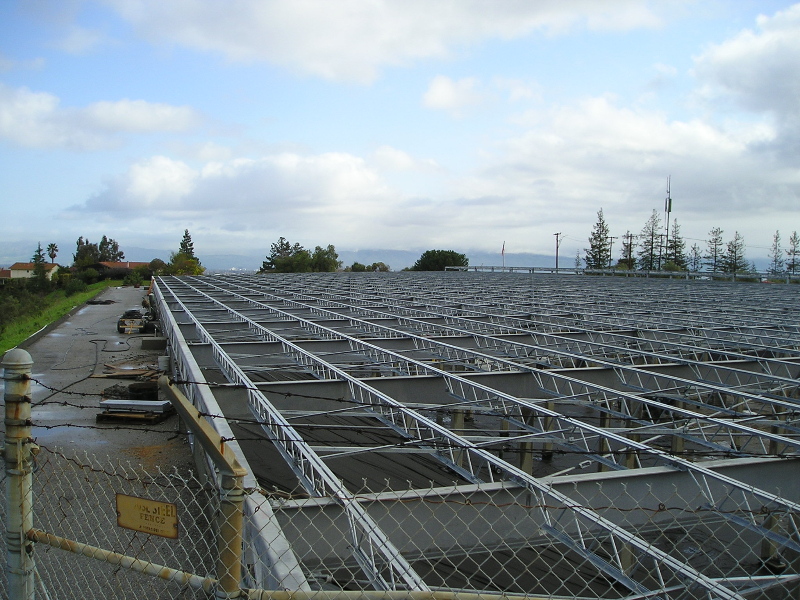
A large field of galvanized solar carport racking under an open sky
Solar racking
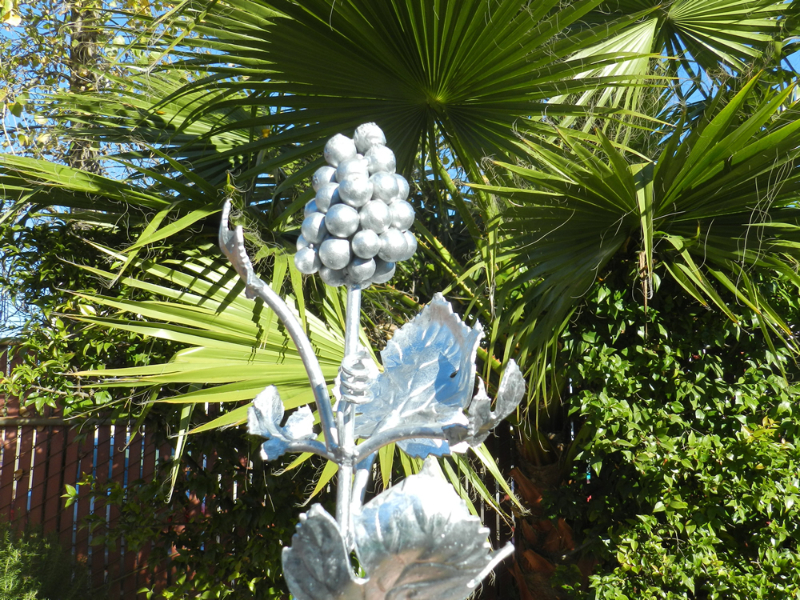
A decorative galvanized steel grapevine sculpture with leaves and a cluster of grapes
Ornamental work
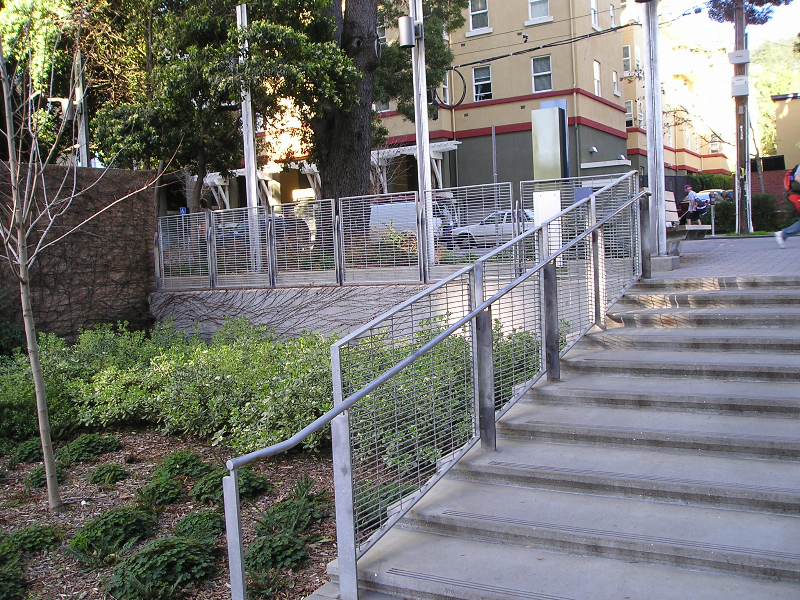
Galvanized handrail and infill guardrail along a set of campus steps
Handrail & guardrail
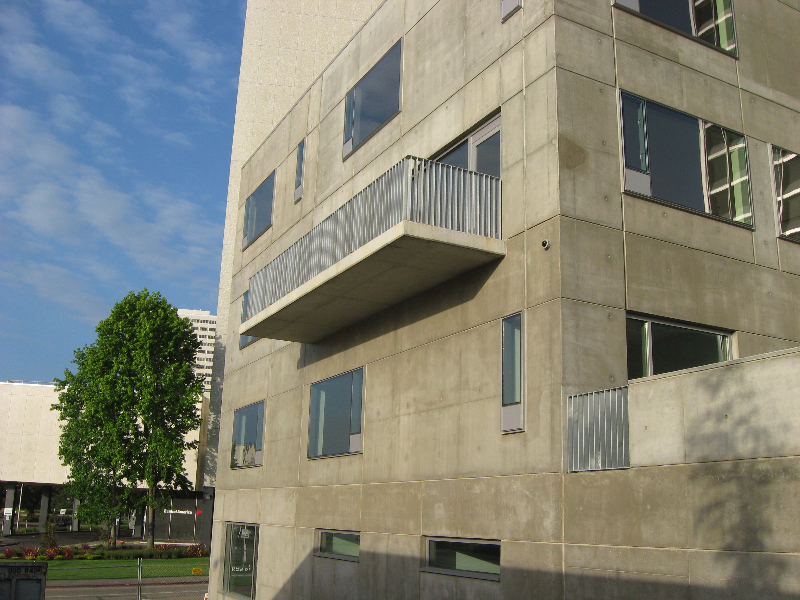
Galvanized balcony railing and window screens on a concrete building
Architectural rail
Galvanized rooftop structural steel between two buildings
Structural steel

Quality

What we hold ourselves to.

Court Galvanizing is committed to continuously providing quality products to our customers, and to continuously improving the hot-dip galvanizing services that meet customer and regulatory requirements.

American Galvanizers Association
A proud member in good standing.

  • The management team and all of our employees are committed to the quality of our hot-dip galvanizing services and our stated quality objectives.
  • We strive to achieve our industry's leading position in providing our customers, at a competitive price, the highest quality of surface preparation and hot-dip galvanizing.
  • We strive to meet all applicable standards and regulations, and any specific customer requirements within the scope of our Quality Management System.
  • We strive to meet or exceed our customers' needs, expectations and satisfaction.
  • We strive to promote a culture of continuous improvement of our galvanizing services and our quality management system.
  • The management team periodically reviews the performance of our quality management system and our quality objectives, to ensure their effectiveness and continuing suitability.

Contact

Talk to us about your job.

Plant 4937 Allison Parkway
Vacaville, California 95688
Phone 707-448-4848
Fax 707-448-4890
Bill Armstrong
Sales & General Manager
billarmstrong@courtgalvanizinginc.com
Jan Reid
Plant Manager
janreid@courtgalvanizinginc.com